Why Filament Absorbs Moisture and Ruins Prints

Why Filament Absorbs Moisture and Ruins Prints

A spool can look perfectly fine on the rack and still be the reason your next print hisses, strings, blisters, or snaps. Understanding why filament absorbs moisture gives you a direct path to cleaner surfaces, stronger parts, and fewer frustrating failures. For makers who expect reliable results, dry filament is not a finishing detail. It is part of the print setup.

Why Filament Absorbs Moisture

Most 3D printing filaments are polymers, and many polymer chains naturally attract water molecules from the air. This behavior is called hygroscopy. It does not mean your spool is defective. It means the material is interacting with its environment exactly as its chemistry allows.

Water vapor is everywhere. A climate-controlled workshop, a garage after a rainstorm, and a shelf near an open window all contain moisture in the air. Once a spool is unsealed, that moisture can gradually move into the filament. The rate depends on the filament type, the local humidity, temperature, and how long the spool has been exposed.

Some materials hold onto water more aggressively than others. TPU is especially moisture-sensitive because of its flexible chemical structure. PETG also pulls in moisture readily, while ABS can absorb enough to affect printing when left out for extended periods. PLA generally absorbs moisture more slowly, but slow does not mean immune. A PLA Pro spool can still lose its crisp performance after sitting exposed in a humid space.

Think of the filament as a material that is always balancing with the air around it. The wetter the air and the longer the exposure, the more likely that balance shifts in the wrong direction for printing.

What Moisture Does Inside a Hotend

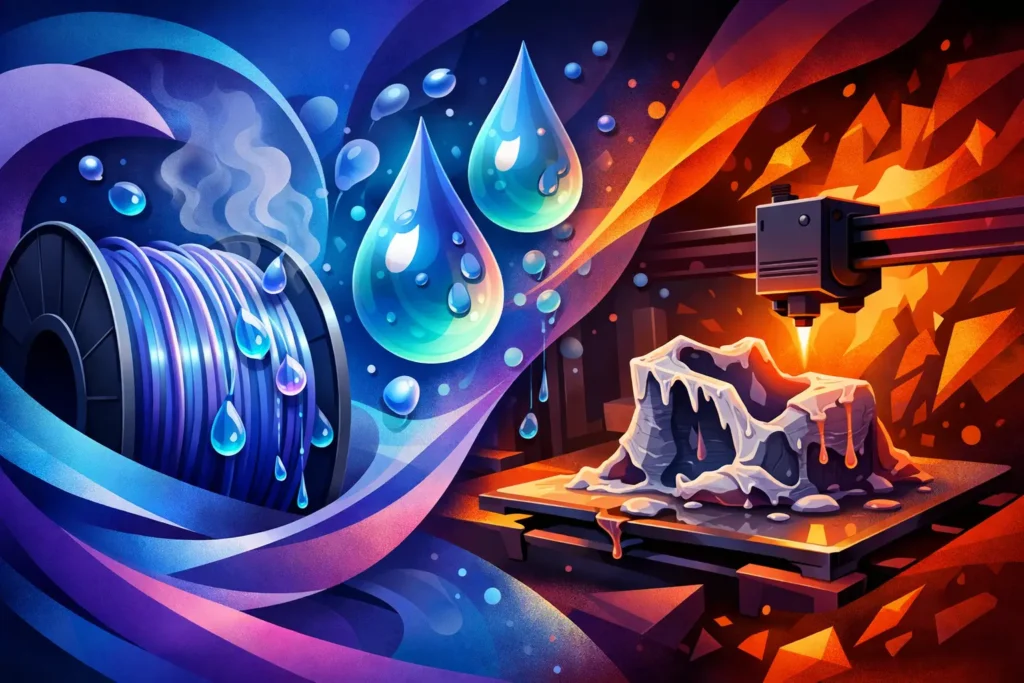
The real trouble starts when damp filament enters a hot nozzle. As the polymer melts, trapped water rapidly turns to steam. Steam expands, creating tiny disruptions in the molten plastic just before it exits the nozzle.

That disruption shows up in ways makers know immediately: popping or sizzling sounds, inconsistent extrusion, rough textures, visible pitting, excessive stringing, and weak layer bonding. In severe cases, the filament may bubble as it leaves the nozzle, leaving a foamy or scarred surface that no amount of tuning can fully hide.

Moisture can also chemically degrade certain polymers under heat. Water molecules can break down polymer chains during melting, reducing the material’s molecular weight. The result can be more brittle parts, less predictable flow, and strength that falls short of what the filament should deliver. This is especially relevant when you are printing functional brackets, flexible components, prototypes, or parts that need to survive real use.

That is why a wet spool often gets blamed on the printer. You may spend an hour adjusting retraction, temperature, flow, and pressure advance, only to find that the issue was moisture all along. Settings matter, but they cannot compensate for water boiling out of the material.

How Moisture Looks Different Across Filament Types

Every material gives you clues, although the clues are not always identical.

PLA and PLA Pro

PLA is often viewed as low-maintenance, and compared with TPU or nylon, it is. Still, long exposure to humidity can create brittle filament, inconsistent extrusion, and a dull or rough finish. PLA Pro is formulated for stronger, more dependable prints, so starting with dry material helps you get the mechanical performance and smooth finish you bought it for.

If your PLA suddenly snaps while feeding from the spool, moisture may be part of the story. Age, UV exposure, and poor storage can also contribute, so treat brittleness as a reason to inspect the whole storage routine rather than assuming one cause.

PETG

PETG is a maker favorite for tough, practical parts, but it is notably prone to moisture-related stringing and surface imperfections. A damp PETG spool may produce wispy strings that seem impossible to tune out. It can also create tiny bumps or pits that are especially obvious on transparent colors and glossy surfaces.

Dry PETG will not eliminate every string by itself. Retraction, travel behavior, nozzle temperature, and cooling still matter. But it gives you a clean baseline for tuning instead of asking your slicer to solve a material problem.

TPU

TPU has a reputation for drinking moisture, and that reputation is earned. Its flexible nature makes it useful for phone grips, bumpers, gaskets, feet, and impact-resistant parts, but it also makes moisture control essential. Wet TPU commonly hisses at the nozzle, creates a rough finish, and extrudes inconsistently.

Because flexible filament already requires controlled feeding, moisture adds another variable you do not need. Keep TPU sealed whenever possible, and consider printing directly from a dry box if your workspace stays humid.

ABS

ABS is generally less thirsty than TPU or PETG, but it should not be left open indefinitely. Moisture can lead to poor surface quality and inconsistent extrusion. ABS already demands attention to chamber temperature, drafts, and warping, so dry filament removes one preventable source of trouble.

Signs Your Filament Needs Drying

You do not need lab equipment to catch most moisture issues. Listen to the nozzle and inspect the print. Popping, crackling, or a faint sizzle during extrusion are strong warning signs, especially with PETG and TPU. So are random strings, a sandy-looking finish, small craters, bubbles, and extrusion that appears to pulse instead of flowing smoothly.

Mechanical changes matter too. Filament that has become unusually brittle, weak prints with poor layer adhesion, or a spool that prints worse than it did a few weeks ago all deserve attention. Of course, a worn nozzle, partial clog, incorrect temperature, or poor spool path can create similar symptoms. Before changing everything at once, test one variable at a time.

A simple diagnostic move is to dry the filament and print the same small test again with unchanged slicer settings. If the surface cleans up and extrusion becomes quieter and steadier, you found a major part of the problem.

Drying Filament Without Damaging It

Drying works because warm, controlled airflow helps moisture leave the filament. The goal is not to cook the spool. Excessive heat can soften filament, fuse neighboring coils together, deform cardboard spools, or make the material harder to feed.

A dedicated filament dryer is the easiest option for regular printing. It is built to hold a spool at controlled temperatures and is practical for makers who rotate through PETG, TPU, and other moisture-sensitive materials. A food dehydrator can also work well if it can maintain a suitable low temperature and has enough space for the spool. An oven is possible, but it is the least forgiving option because many household ovens fluctuate more than their displays suggest.

Drying time and temperature depend on the material, spool size, and how wet it is. As a conservative starting point, use low heat for PLA, moderate heat for PETG and TPU, and follow the material supplier’s recommended range when available. Check the spool’s heat tolerance before using any drying method. A temperature that is safe for one spool or material may be risky for another.

Do not judge dryness only by the clock. Run a short print after drying. Quiet extrusion, smoother walls, reduced stringing, and more consistent flow are the results that count.

Storage Is the Real Print-Quality Upgrade

Drying saves a wet spool. Storage keeps it from becoming wet again. The most effective routine is simple: return filament to an airtight container or resealable bag as soon as the print is done. Add fresh desiccant packs, and replace or recharge them when their indicator shows they are saturated.

For a small collection, heavy-duty zipper bags and desiccant are a strong, affordable solution. For a larger material lineup, sealed storage bins make it easier to organize colors and materials while protecting multiple spools at once. A humidity indicator card inside the container gives you an immediate read on whether your storage system is doing its job.

If you print often, a dry box that feeds filament directly to the printer is worth considering. It reduces the time a spool spends exposed between projects, which matters most for TPU and PETG. The trade-off is convenience versus setup space and cost. A sealed bag works fine for occasional makers who build a consistent habit around it.

Keep unopened spools sealed until you are ready to use them. Once opened, label the bag or container with the material and date. That small step makes it easier to spot which spools have been sitting through a wet season or a long project break.

Build Your Process Around Dry Material

Reliable prints come from controlling the variables you can control. Level the bed, use a clean nozzle, choose sensible slicer settings, and protect the material before it reaches the hotend. When a spool is dry, you can tune for the qualities that matter: smooth walls, accurate dimensions, dependable strength, and a finish you are proud to show off.

Ddub Tech filaments are built for makers who want stronger, smoother, more reliable results. Give every spool the same advantage with smart storage and timely drying. Your next great print should be shaped by your design, not by the humidity in your room.
Leave a Comment

Your email address will not be published. Required fields are marked *

Why Filament Absorbs Moisture and Ruins Prints

Why Filament Absorbs Moisture and Ruins Prints

A spool can look perfectly fine on the rack and still be the reason your next print hisses, strings, blisters, or snaps. Understanding why filament absorbs moisture gives you a direct path to cleaner surfaces, stronger parts, and fewer frustrating failures. For makers who expect reliable results, dry filament is not a finishing detail. It is part of the print setup.

Why Filament Absorbs Moisture

Most 3D printing filaments are polymers, and many polymer chains naturally attract water molecules from the air. This behavior is called hygroscopy. It does not mean your spool is defective. It means the material is interacting with its environment exactly as its chemistry allows.

Water vapor is everywhere. A climate-controlled workshop, a garage after a rainstorm, and a shelf near an open window all contain moisture in the air. Once a spool is unsealed, that moisture can gradually move into the filament. The rate depends on the filament type, the local humidity, temperature, and how long the spool has been exposed.

Some materials hold onto water more aggressively than others. TPU is especially moisture-sensitive because of its flexible chemical structure. PETG also pulls in moisture readily, while ABS can absorb enough to affect printing when left out for extended periods. PLA generally absorbs moisture more slowly, but slow does not mean immune. A PLA Pro spool can still lose its crisp performance after sitting exposed in a humid space.

Think of the filament as a material that is always balancing with the air around it. The wetter the air and the longer the exposure, the more likely that balance shifts in the wrong direction for printing.

What Moisture Does Inside a Hotend

The real trouble starts when damp filament enters a hot nozzle. As the polymer melts, trapped water rapidly turns to steam. Steam expands, creating tiny disruptions in the molten plastic just before it exits the nozzle.

That disruption shows up in ways makers know immediately: popping or sizzling sounds, inconsistent extrusion, rough textures, visible pitting, excessive stringing, and weak layer bonding. In severe cases, the filament may bubble as it leaves the nozzle, leaving a foamy or scarred surface that no amount of tuning can fully hide.

Moisture can also chemically degrade certain polymers under heat. Water molecules can break down polymer chains during melting, reducing the material’s molecular weight. The result can be more brittle parts, less predictable flow, and strength that falls short of what the filament should deliver. This is especially relevant when you are printing functional brackets, flexible components, prototypes, or parts that need to survive real use.

That is why a wet spool often gets blamed on the printer. You may spend an hour adjusting retraction, temperature, flow, and pressure advance, only to find that the issue was moisture all along. Settings matter, but they cannot compensate for water boiling out of the material.

How Moisture Looks Different Across Filament Types

Every material gives you clues, although the clues are not always identical.

PLA and PLA Pro

PLA is often viewed as low-maintenance, and compared with TPU or nylon, it is. Still, long exposure to humidity can create brittle filament, inconsistent extrusion, and a dull or rough finish. PLA Pro is formulated for stronger, more dependable prints, so starting with dry material helps you get the mechanical performance and smooth finish you bought it for.

If your PLA suddenly snaps while feeding from the spool, moisture may be part of the story. Age, UV exposure, and poor storage can also contribute, so treat brittleness as a reason to inspect the whole storage routine rather than assuming one cause.

PETG

PETG is a maker favorite for tough, practical parts, but it is notably prone to moisture-related stringing and surface imperfections. A damp PETG spool may produce wispy strings that seem impossible to tune out. It can also create tiny bumps or pits that are especially obvious on transparent colors and glossy surfaces.

Dry PETG will not eliminate every string by itself. Retraction, travel behavior, nozzle temperature, and cooling still matter. But it gives you a clean baseline for tuning instead of asking your slicer to solve a material problem.

TPU

TPU has a reputation for drinking moisture, and that reputation is earned. Its flexible nature makes it useful for phone grips, bumpers, gaskets, feet, and impact-resistant parts, but it also makes moisture control essential. Wet TPU commonly hisses at the nozzle, creates a rough finish, and extrudes inconsistently.

Because flexible filament already requires controlled feeding, moisture adds another variable you do not need. Keep TPU sealed whenever possible, and consider printing directly from a dry box if your workspace stays humid.

ABS

ABS is generally less thirsty than TPU or PETG, but it should not be left open indefinitely. Moisture can lead to poor surface quality and inconsistent extrusion. ABS already demands attention to chamber temperature, drafts, and warping, so dry filament removes one preventable source of trouble.

Signs Your Filament Needs Drying

You do not need lab equipment to catch most moisture issues. Listen to the nozzle and inspect the print. Popping, crackling, or a faint sizzle during extrusion are strong warning signs, especially with PETG and TPU. So are random strings, a sandy-looking finish, small craters, bubbles, and extrusion that appears to pulse instead of flowing smoothly.

Mechanical changes matter too. Filament that has become unusually brittle, weak prints with poor layer adhesion, or a spool that prints worse than it did a few weeks ago all deserve attention. Of course, a worn nozzle, partial clog, incorrect temperature, or poor spool path can create similar symptoms. Before changing everything at once, test one variable at a time.

A simple diagnostic move is to dry the filament and print the same small test again with unchanged slicer settings. If the surface cleans up and extrusion becomes quieter and steadier, you found a major part of the problem.

Drying Filament Without Damaging It

Drying works because warm, controlled airflow helps moisture leave the filament. The goal is not to cook the spool. Excessive heat can soften filament, fuse neighboring coils together, deform cardboard spools, or make the material harder to feed.

A dedicated filament dryer is the easiest option for regular printing. It is built to hold a spool at controlled temperatures and is practical for makers who rotate through PETG, TPU, and other moisture-sensitive materials. A food dehydrator can also work well if it can maintain a suitable low temperature and has enough space for the spool. An oven is possible, but it is the least forgiving option because many household ovens fluctuate more than their displays suggest.

Drying time and temperature depend on the material, spool size, and how wet it is. As a conservative starting point, use low heat for PLA, moderate heat for PETG and TPU, and follow the material supplier’s recommended range when available. Check the spool’s heat tolerance before using any drying method. A temperature that is safe for one spool or material may be risky for another.

Do not judge dryness only by the clock. Run a short print after drying. Quiet extrusion, smoother walls, reduced stringing, and more consistent flow are the results that count.

Storage Is the Real Print-Quality Upgrade

Drying saves a wet spool. Storage keeps it from becoming wet again. The most effective routine is simple: return filament to an airtight container or resealable bag as soon as the print is done. Add fresh desiccant packs, and replace or recharge them when their indicator shows they are saturated.

For a small collection, heavy-duty zipper bags and desiccant are a strong, affordable solution. For a larger material lineup, sealed storage bins make it easier to organize colors and materials while protecting multiple spools at once. A humidity indicator card inside the container gives you an immediate read on whether your storage system is doing its job.

If you print often, a dry box that feeds filament directly to the printer is worth considering. It reduces the time a spool spends exposed between projects, which matters most for TPU and PETG. The trade-off is convenience versus setup space and cost. A sealed bag works fine for occasional makers who build a consistent habit around it.

Keep unopened spools sealed until you are ready to use them. Once opened, label the bag or container with the material and date. That small step makes it easier to spot which spools have been sitting through a wet season or a long project break.

Build Your Process Around Dry Material

Reliable prints come from controlling the variables you can control. Level the bed, use a clean nozzle, choose sensible slicer settings, and protect the material before it reaches the hotend. When a spool is dry, you can tune for the qualities that matter: smooth walls, accurate dimensions, dependable strength, and a finish you are proud to show off.

Ddub Tech filaments are built for makers who want stronger, smoother, more reliable results. Give every spool the same advantage with smart storage and timely drying. Your next great print should be shaped by your design, not by the humidity in your room.
Leave a Comment

Your email address will not be published. Required fields are marked *

RSS
Follow by Email
Tiktok
0