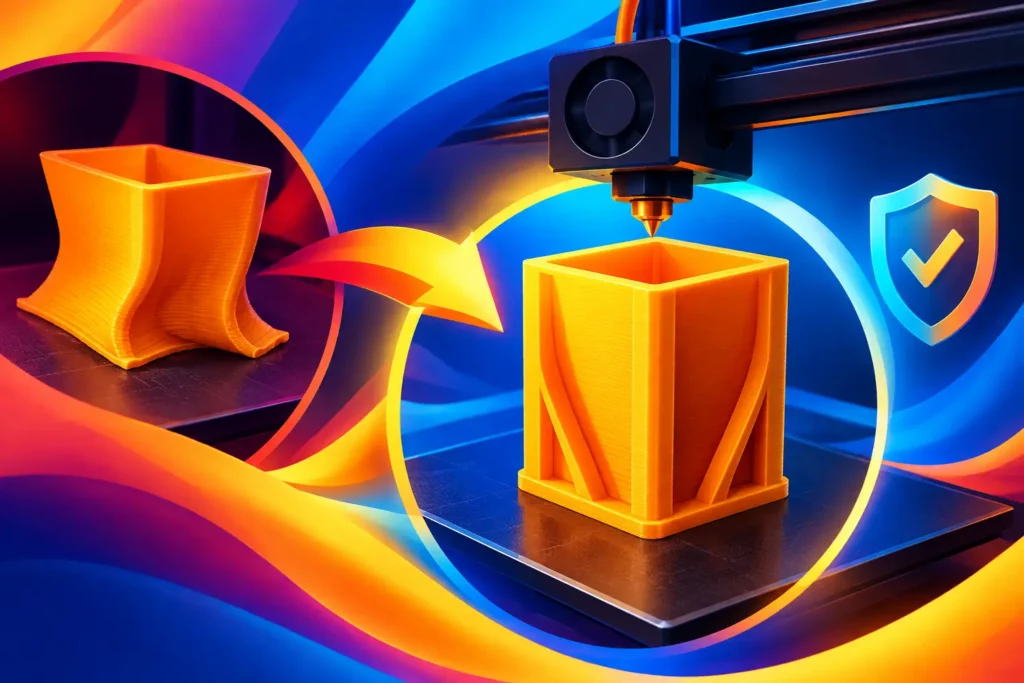
A lifted corner can ruin an otherwise perfect ABS part in the final hour of a print. The fix is rarely one magic setting. Learning how to prevent ABS warping means controlling the temperature changes that make this strong, heat-resistant material shrink as it cools. Get that environment right, and ABS becomes far less intimidating – and far more capable.
Why ABS Warps in the First Place
ABS contracts as it cools. Every printed layer wants to get slightly smaller than it was when it left the nozzle. On a small, simple part, that movement may not be enough to cause trouble. On a large flat bracket, enclosure, tool holder, or functional prototype, the internal pull can overpower bed adhesion and lift the edges.
That is why warping is often worse on prints with broad first layers, sharp corners, and long straight walls. The bottom layers are held to the build plate while upper layers cool and shrink. The result is stress that builds upward and outward until a corner curls or the entire part releases.
ABS does not need a mysterious process. It needs stable heat. Cold drafts, an underpowered bed, poor first-layer contact, and aggressive cooling all make the material fight itself. Your goal is to keep the part warm enough, long enough, for it to cool gradually instead of unevenly.
How to Prevent ABS Warping With Stable Heat
An enclosure is the biggest upgrade most ABS users can make. It traps the warmth produced by the heated bed and hotend, reducing the temperature gap between the first layer and the layers printed later. For many consumer printers, an enclosure temperature around 95 to 120°F is a practical starting range.
You do not need to overheat the printer. Too much chamber heat can soften filament before it reaches the extruder gears, strain stepper motors, or create problems for electronics that were not designed to operate in a hot enclosed space. Keep sensitive electronics outside the enclosure when possible, follow your printer manufacturer’s safety guidance, and monitor temperatures during early tests.
Your heated bed matters just as much. ABS commonly prints well with a bed set around 100 to 110°C. Start near the middle of that range, then adjust based on what you see. If the bottom corners are lifting, raise the bed temperature slightly. If the first layer looks overly soft, spreads too much, or develops a rough elephant-foot edge, reduce it a few degrees.
Nozzle temperature also affects warping. A nozzle that is too cool can produce weak layer bonding, while one that is too hot can make fine features soft and messy. Many ABS filaments run well around 230 to 260°C, but the correct window depends on the specific spool, nozzle, print speed, and printer. Start with the filament maker’s recommendation, then change only one variable at a time.
Ambient conditions count. Do not print ABS next to an open window, air-conditioning vent, fan, or garage door that opens every few minutes. Even a small draft can cool one side of a print faster than the other. If you cannot use a full enclosure, a draft shield in your slicer can help, but it is not a replacement for controlled chamber heat.
Build a First Layer That Will Not Let Go
A perfectly heated printer still needs a first layer with real grip. Start with a clean build surface. Finger oils, dust, and residue from previous prints reduce adhesion fast. Wash the plate according to its material and manufacturer guidance, then avoid touching the print area with bare hands.
The right build surface depends on your setup. Textured PEI, smooth PEI with an appropriate release layer, garolite, and ABS slurry systems can all work. The trade-off is release behavior. ABS can bond extremely hard to some surfaces, so use a compatible barrier or adhesive when needed to protect the plate and make part removal predictable.
Leveling and Z-offset deserve more attention than they usually get. The first line should look gently pressed into the surface, with no gaps between neighboring lines. If the nozzle is too high, the filament sits on top of the plate and can peel away. If it is too low, the nozzle may drag, restrict flow, and create a rough first layer that introduces stress before the print even begins.
For a large ABS part, slow the first layer to roughly 15 to 25 mm/s. This gives the plastic time to transfer heat into the bed and form a solid bond. A first-layer height around 0.2 to 0.28 mm with a 0.4 mm nozzle is a dependable place to start, provided your printer is properly calibrated.
Use Slicer Settings That Work With ABS
Turn the part-cooling fan off for the first several layers. In a warm enclosure, many ABS prints can run with the fan off for the entire job. That preserves layer bonding and reduces the sudden cooling that triggers curling.
There are exceptions. Small overhangs, bridges, and fine pointed features may benefit from a small amount of airflow. If your geometry needs it, use the lowest fan setting that produces clean detail, such as 10 to 20 percent, rather than blasting the print with full cooling. Keep the fan off or near off for large structural walls and broad flat surfaces.
A brim is one of the easiest ways to add insurance. It creates a wide, single-layer skirt attached to the part’s perimeter, increasing contact area exactly where corners want to lift. A brim of 8 to 15 mm is often enough for medium-size functional parts. For very large or stubborn prints, go wider.
Rafts can also work, but they use more material, add cleanup, and can leave a rougher underside. Save them for parts with tiny contact points or geometry that refuses to stay down even after your bed setup is dialed in. For most ABS projects, a properly tuned brim is the cleaner solution.
Avoid printing large flat objects with 100 percent infill unless the part truly requires it. Dense infill creates more shrinking force inside the model. Lower infill, sensible wall counts, and well-designed ribs can often deliver a strong part with less stress. For functional prints, two to four walls and moderate infill are usually more useful than simply packing the entire model solid.
Match Part Design to ABS Behavior
Sharp outside corners concentrate stress. If you are designing the model yourself, add small fillets or chamfers where possible. Rounded corners spread stress more evenly and are less likely to lift. A part with a huge flat bottom is inherently harder to print in ABS than one broken into smaller sections or redesigned with ribs and relief features.
Orientation makes a difference too. Put the most stable, least warp-prone face on the bed when the part’s strength requirements allow it. If a wide panel must be printed flat, expect to use a brim, a warm enclosure, and careful bed preparation. If it can be printed on its side with supports, the trade-off may be a cleaner first layer and much lower warping risk.
Do Not Ignore Filament Condition
Moisture is not the main cause of ABS warping, but wet ABS can make everything harder to tune. It may pop at the nozzle, leave rough surfaces, and produce inconsistent extrusion that weakens the first layer. Keep spools sealed with desiccant when not in use, and dry questionable filament before chasing slicer settings.
Quality, consistent filament helps because temperature tuning becomes repeatable. When every spool behaves differently, it is difficult to know whether the issue is your printer, your environment, or the material. Performance-focused ABS from Ddub Tech gives makers a dependable starting point for strong, clean functional prints.
Read the Failure Before Changing Settings
If only one corner lifts, look first for a draft, uneven bed heating, or a dirty spot on the plate. If every corner lifts, the chamber is likely too cool, the bed temperature is too low, or the first layer is not pressed in enough. If the print stays down for hours and then cracks up the side, the issue is usually rapid cooling or too much fan rather than adhesion alone.
Make changes methodically. Do not raise the nozzle temperature, bed temperature, brim width, and enclosure temperature all at once. Print a simple flat test piece, adjust one factor, and compare the result. That is how you turn ABS from a string of guesses into a repeatable material process.
ABS rewards control. Give it a clean, well-tuned first layer and a calm, warm space to cool, then let it do what it does best: produce tough parts that are ready for real work.