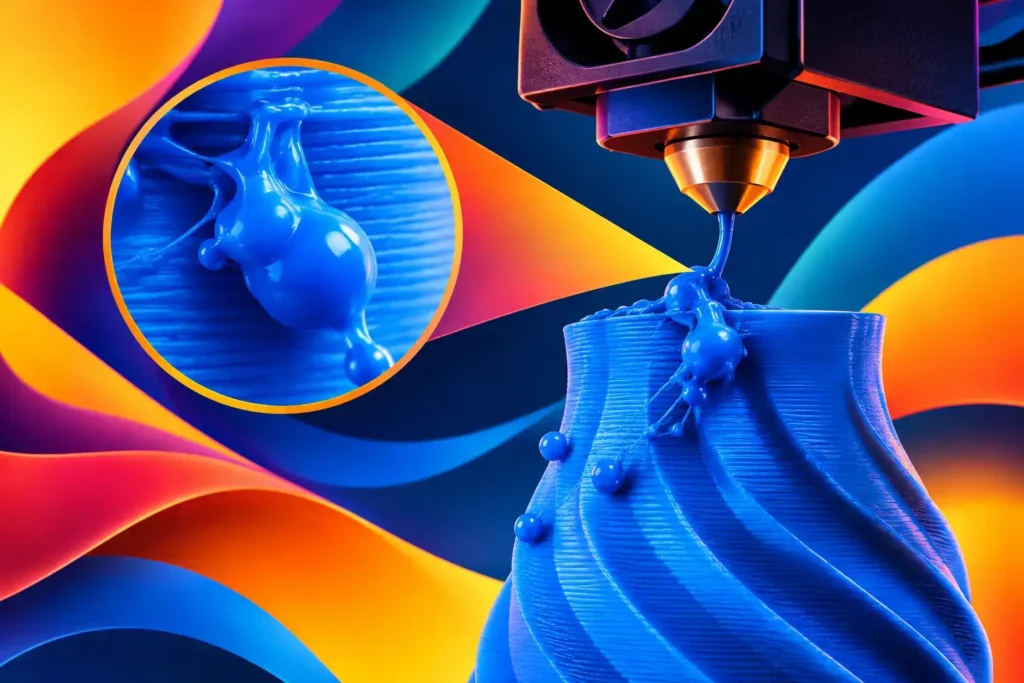
A single PETG blob can turn an otherwise clean print into a part that looks unfinished. You may see a small zit at every layer change, a stringy lump on a vertical wall, or a buildup of plastic around the nozzle that eventually lands on the model. So, what causes PETG blobs? Usually, it is not one bad setting. It is excess molten filament escaping from the nozzle at the wrong moment.
PETG is strong, durable, and an excellent choice for functional prints, but it stays tacky and fluid longer than PLA. That is part of why it bonds so well between layers. It also means your printer needs better control over heat, pressure, retraction, and filament condition. The good news: blobs are a tuning problem you can solve without giving up the material you want to print.
What Causes PETG Blobs During a Print?
A blob forms when the nozzle deposits more material than the toolpath expects, or when it drags softened plastic across a finished surface. That extra material may come from internal nozzle pressure, wet filament, an overheated melt zone, poor travel behavior, or an imperfect first layer. Sometimes the printer is also creating the problem mechanically with a dirty nozzle, loose hotend components, or a partial clog.
The shape and location of the blob offer useful clues. Small, repeating zits in one vertical line usually point to the seam or pressure control. Random pops and rough spots across the whole print often point to moisture. A large mass that grows around the nozzle is more urgent, because it can catch on the part and cause a full print failure.
Before changing five settings at once, inspect the print and make one controlled adjustment. PETG rewards a methodical approach.
Wet Filament Creates Random PETG Zits
PETG absorbs moisture from the air. Once moisture reaches the hotend, it turns to steam and expands, causing tiny bursts in the melted filament. The result can be popping sounds, wispy strings, surface pitting, inconsistent extrusion, and random blobs.
This can happen even when a spool looks fine. A spool left out for a few humid days may still feed normally while producing a rougher surface than expected. Transparent PETG can make the issue especially easy to see because bubbles and texture show up clearly in the finished part.
Dry the filament before chasing slicer settings. Use a filament dryer or a temperature-controlled drying setup intended for filament, then store the spool in a sealed container with desiccant. If a previously reliable PETG spool suddenly starts popping and leaving scattered defects, drying is the first move worth making.
Temperature Can Make PETG Too Runny
PETG needs enough heat to flow smoothly and create strong layer adhesion. Push the nozzle temperature too high, however, and the melt becomes overly fluid. It oozes during travel moves, hangs from the nozzle, and leaves behind blobs when the printer slows down or changes direction.
Start within the temperature range recommended for your specific filament, then print a temperature tower or a small test model. Lower the nozzle temperature in small increments, usually 5 degrees at a time, until stringing and blobs improve without sacrificing layer bonding or creating under-extrusion.
Cooling matters too. PETG generally prefers less fan than PLA, but zero cooling is not always the answer. On small layers or detailed sections, a modest amount of part cooling helps plastic set before the nozzle comes back around. Too much fan can weaken layer adhesion or cause warping, so tune for the part you are making. A bracket and a decorative figurine do not need identical settings.
Retraction Settings and Nozzle Pressure Matter
When a travel move begins, the printer retracts filament to reduce ooze. If retraction is too low, too slow, or delayed, PETG continues leaking from the nozzle. When printing resumes, the extra material can settle into a zit or get dragged across the wall.
But more retraction is not automatically better. PETG is prone to grinding and heat creep when retraction distance or speed gets aggressive, especially on a direct-drive printer. Excessive retractions can also create inconsistent starts after travel moves. Tune in small steps and match the approach to your extruder design. Bowden systems typically need more distance than direct-drive systems.
Pressure advance or linear advance is another major factor. The nozzle contains pressurized molten plastic while printing. At corners, speed changes, and the end of a line, that pressure does not disappear instantly. Pressure advance compensates for the delay, reducing bulges at line endings and seam locations. If your printer supports it, calibrating this setting can make a dramatic difference on PETG walls.
The Z Seam Is Often the Real Culprit
If every blob appears in a nearly straight vertical line, your PETG may be printing correctly everywhere except where each layer starts and stops. That line is the Z seam. A seam is unavoidable on most FDM prints, but it can be hidden, aligned intentionally, or distributed depending on the model and slicer settings.
Placing the seam on a sharp rear corner is often the cleanest option for functional parts. For rounded objects, a scattered seam may prevent one obvious vertical scar, though it can spread small zits around the surface. Neither choice is universally best. Choose based on where the finished part will be seen and how much post-processing it can tolerate.
Wipe settings can also help. Wiping moves the nozzle slightly while retracting, which relieves pressure before the travel move. Combined with a tuned retraction and pressure advance value, it can noticeably reduce seam blobs.
Travel Moves, Speed, and Acceleration Can Leave Blobs
PETG loves to stick, including to the nozzle. If travel paths cross printed surfaces while the nozzle is oozing, it may drag a small strand until it cools into a lump. Enable travel behavior that avoids crossing external walls when practical, and use a travel speed your printer can handle consistently.
Very slow travel moves give hot PETG more time to ooze. Very high acceleration can make the machine overshoot or vibrate, leaving marks at direction changes. Print speed has a similar trade-off. Faster printing can increase pressure in the nozzle, while slower printing can increase dwell time and heat buildup. The goal is not the biggest number in your slicer. It is stable extrusion with clean movement.
If blobs show up around tiny features, minimum layer time may be involved. The hotend keeps passing over the same small area before it has time to set. Slowing small layers and adding controlled cooling can help the part hold its shape without turning PETG brittle.
Hardware Problems That Look Like Slicer Problems
Do not overlook the hotend. A nozzle with burnt residue can collect PETG and smear it onto the print. A partial clog creates irregular pressure and intermittent over-extrusion. A worn nozzle can change the actual opening size enough to throw off flow.
Check that the nozzle is clean and properly tightened against the heat break while the hotend is at the correct assembly temperature. If molten plastic is leaking from above the heater block, stop the print and fix the hotend seal. That leak can build into a large blob around the nozzle and damage the heater, thermistor wires, or the print itself.
Also confirm your extrusion multiplier or flow rate. Over-extrusion makes every problem louder: seams swell, corners bulge, and nozzle buildup increases. Calibrate extrusion before trying to compensate with extreme retraction values.
A Smart Order for Fixing PETG Blobs
Start with the highest-probability causes instead of rebuilding your entire profile. Dry the spool, clean the nozzle, and verify that the hotend is not leaking. Then tune temperature and flow. Once extrusion is stable, adjust retraction, pressure advance, wipe behavior, seam placement, and travel settings.
Use the same small test print after each change. A simple model with walls, corners, travel gaps, and a visible seam reveals more than a long print that takes eight hours to finish. Keep notes on the values that work for each PETG color and brand, because pigments and additives can change behavior slightly.
Quality filament makes this process far less frustrating. Consistent diameter and clean winding give your extruder a predictable job, while well-dried, performance-focused PETG gives you a stronger starting point. Ddub Tech PETG is built for makers who want durable parts and smoother results without turning every project into a troubleshooting session.
PETG blobs are not a sign that you picked the wrong material. They are your printer telling you that heat, moisture, pressure, or movement needs attention. Make one measured change, watch what the surface tells you, and the clean, strong prints you wanted will start showing up layer by layer.